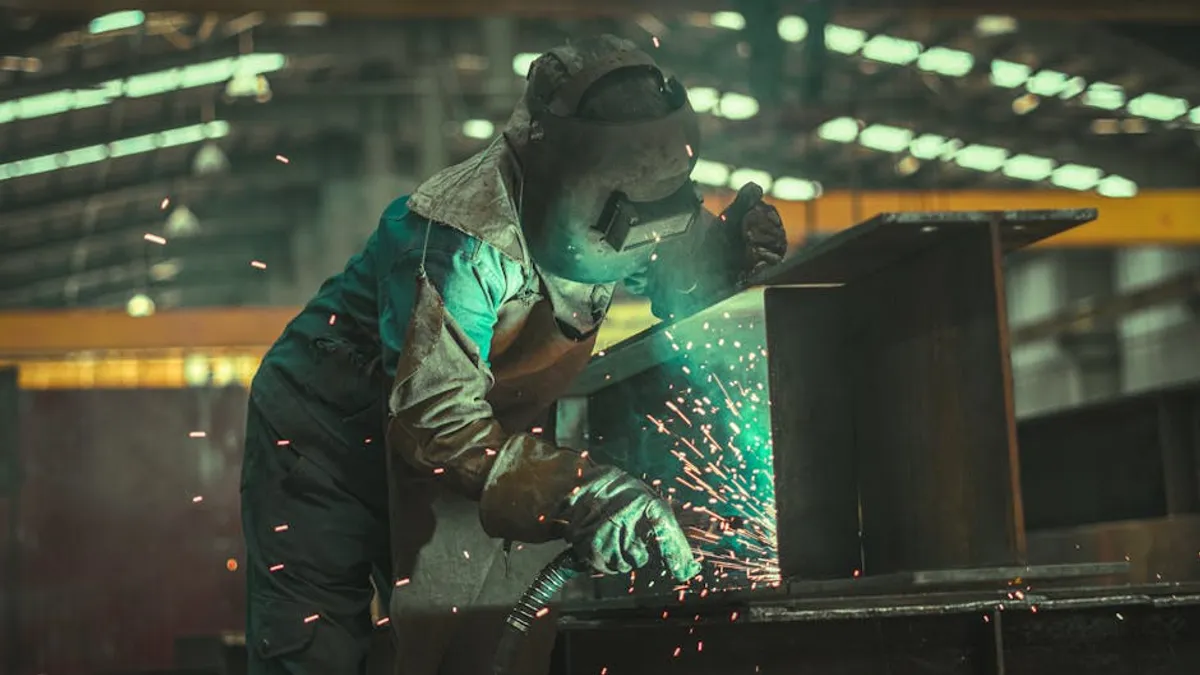
Achieving high-quality MIG welds depends on several factors, and among the most critical is the precise management of shielding gas pressure. Incorrect gas flow leads to compromised weld integrity, increased material waste, and inefficient operation. This guide details the principles of MIG welding gas pressure, covering gas types, equipment specifications, and practical advice for optimizing your setup to ensure consistent, strong welds while managing operational costs effectively.
Understanding Shielding Gas in MIG Welding
Shielding gas protects the molten weld pool and the electrode from atmospheric contamination, specifically oxygen and nitrogen. Without adequate shielding, the weld becomes porous, brittle, and weak. The gas creates an inert or semi-inert envelope around the arc and molten metal, preventing reactions that would otherwise degrade the weld's mechanical properties and appearance.
The choice of shielding gas and its flow rate directly influences arc stability, penetration profile, spatter levels, and the final mechanical properties of the weld. Different materials and welding applications require specific gas compositions to achieve optimal results.
Common Shielding Gas Types and Their Applications
- Argon (Ar): An inert gas, primarily used for welding aluminum, magnesium, copper, and other non-ferrous metals. It produces a stable arc, good penetration, and minimal spatter. Pure argon is also suitable for spray transfer on stainless steel.
- Carbon Dioxide (CO2): An active gas, economical and effective for welding carbon steel. It provides deep penetration but tends to produce more spatter and a harsher arc compared to argon blends. Often used for heavy structural steel work.
- Argon/CO2 Blends: The most common choice for welding carbon steel and some stainless steels. Blends typically range from 75% Argon/25% CO2 to 90% Argon/10% CO2. These blends combine the arc stability of argon with the penetration of CO2, reducing spatter and improving wire feed characteristics over pure CO2.
- Argon/Oxygen Blends: Small additions of oxygen (1-5%) to argon can stabilize the arc and improve wetting action, particularly in spray transfer applications on stainless steel and carbon steel.
Setting the Correct MIG Gas Flow Rate
While gas is stored in a cylinder under high pressure (typically 2000-2200 PSI), the critical operational parameter for MIG welding is the *flow rate*, measured in cubic feet per hour (CFH) or liters per minute (LPM). A regulator reduces the cylinder pressure, and a flowmeter then controls the gas flow to the welding torch. The optimal flow rate ensures sufficient shielding without excessive waste.
Several factors dictate the appropriate flow rate:
- Material Type and Thickness: Thicker materials or those requiring deeper penetration may benefit from slightly higher flow rates to maintain a robust shield.
- Wire Diameter and Stick-Out: Larger wire diameters or longer stick-out (the length of electrode extending beyond the contact tip) can require increased flow.
- Nozzle Size: Larger nozzle diameters generally require higher flow rates to effectively fill the shielding area.
- Welding Position: Out-of-position welding (vertical, overhead) might require a slightly higher flow rate to counteract gravity and maintain shield integrity.
- Ambient Conditions: Drafts, fans, or outdoor welding environments necessitate higher flow rates to prevent atmospheric disturbance from compromising the gas shield.
- Joint Type: Fillet welds or deeply grooved joints may trap gas more effectively, potentially allowing for slightly lower flow rates than open butt joints.
Pro Tip: A common starting point for MIG welding gas flow is 20-30 CFH (9-14 LPM) for most indoor applications with a standard nozzle. Always perform a test weld and visually inspect for porosity or excessive spatter. Adjust flow gradually in 5 CFH (2 LPM) increments until the weld appears clean and stable. Too little gas causes porosity; too much gas can create turbulence, pulling in ambient air, and wasting gas.
MIG Welding Gas Regulators and Flowmeters
The equipment used to control gas flow is crucial for consistent weld quality and efficient gas usage. A regulator reduces high cylinder pressure to a usable working pressure, while a flowmeter measures and controls the actual gas flow rate to the torch.
Types of Equipment
- Single-Stage Regulator with Flowmeter: The most common setup for hobbyists and light industrial use. It reduces cylinder pressure in one step and includes a flow tube or ball-type flowmeter to indicate CFH/LPM.
- Two-Stage Regulator with Flowmeter: Offers more precise and stable control of outlet pressure, which can be beneficial for critical applications or long welding sessions where consistent flow is paramount.
- Heated Regulators: Essential when using pure CO2, especially in colder environments or at high flow rates. CO2 expands rapidly as it leaves the cylinder, causing it to cool significantly and potentially freeze the regulator. A heater prevents this.
- Combination Units: Many modern units integrate the regulator and flowmeter into a single compact device.
Key Specifications for Selection
- Inlet Pressure Range: Must match the maximum pressure of your gas cylinders.
- Outlet Pressure Range: Should be suitable for your welding machine's requirements.
- Flow Rate Capacity: Ensure the flowmeter can accurately measure and control the range of CFH/LPM you need for your applications.
- Material Construction: Brass is common for inert gases. For corrosive gases or specific industrial environments, stainless steel or chrome-plated brass might be preferred for durability.
- Gauge Readability: Clear, easy-to-read gauges for both cylinder pressure and flow rate.
Installation and Maintenance Best Practices
Proper installation and regular maintenance of your gas system prevent leaks, ensure safety, and maintain consistent weld quality.
Installation:
- Secure the gas cylinder upright to prevent tipping.
- Ensure the regulator's inlet connection matches the cylinder valve (e.g., CGA 580 for Argon/Argon blends/CO2).
- Hand-tighten the regulator nut, then use a wrench for a final snug turn, avoiding overtightening.
- Connect the gas hose from the flowmeter to the MIG welder's gas inlet.
- Slowly open the cylinder valve, listening for leaks.
Maintenance:
- Leak Detection: Regularly check all connections using a soapy water solution. Bubbles indicate a leak. Address immediately.
- Gauge Calibration: While not a user-serviceable item, ensure gauges are not damaged and provide consistent readings.
- Hose Inspection: Check gas hoses for cracks, cuts, or wear. Replace damaged hoses promptly.
- Storage: Store gas cylinders in a well-ventilated area, away from heat sources, and secured to prevent falling.
Troubleshooting Common Gas Pressure Issues
Understanding how gas pressure impacts weld defects helps in quick diagnosis and correction:
- Porosity: Often caused by insufficient shielding gas (flow rate too low), gas leaks in the system, excessive wind/draft, or a clogged nozzle. It can also result from too high a flow rate, which creates turbulence.
- Excessive Spatter: While often related to voltage/wire feed speed, high gas flow can sometimes contribute by disrupting the arc. Too little gas can also lead to an unstable arc and more spatter.
- Unstable Arc: Inconsistent gas flow due to leaks, a faulty regulator/flowmeter, or an empty cylinder can cause erratic arc behavior.
- Weld Discoloration/Soot: Especially noticeable on stainless steel, this indicates inadequate shielding, allowing atmospheric oxygen to react with the hot metal. Increase flow rate or address drafts.
Optimizing Your MIG Welding Gas Setup
Effective management of MIG welding gas pressure is an ongoing process of calibration and attention to detail. Consistent, high-quality welds depend on a stable, appropriate gas shield. Regularly verify your flow rate settings for each application, monitor for leaks, and maintain your equipment. This diligence not only ensures superior weld integrity but also optimizes gas consumption, reducing operational costs over time. Investing in a reliable regulator and flowmeter, understanding the nuances of different shielding gases, and adapting your flow rate to environmental conditions are all critical steps toward maximizing your MIG welding efficiency and output quality.
Frequently Asked Questions
What is the ideal MIG welding gas pressure?
The ideal operational parameter is gas flow rate, typically measured in cubic feet per hour (CFH) or liters per minute (LPM), not pressure. A common starting range for MIG welding is 20-30 CFH (9-14 LPM), but this varies based on material, wire size, nozzle size, and environmental conditions.
How do I check for MIG gas leaks?
Spray a solution of soapy water onto all gas connections (cylinder valve, regulator, hose fittings, and torch connection) while the gas is flowing. Bubbles forming indicate a leak. Tighten connections or replace faulty components as necessary.
Can I use pure CO2 for MIG welding?
Yes, pure CO2 is commonly used for welding carbon steel, particularly for applications requiring deep penetration or when cost is a primary concern. However, it generally produces more spatter and a harsher arc than argon/CO2 blends, and a heated regulator may be necessary in colder conditions to prevent freezing.
What is the difference between a regulator and a flowmeter?
A regulator reduces the high pressure from the gas cylinder to a lower, usable working pressure. A flowmeter, often integrated with the regulator, then measures and controls the actual volume of gas flowing to the welding torch per unit of time (e.g., CFH or LPM), ensuring the correct amount of shielding gas reaches the weld pool.